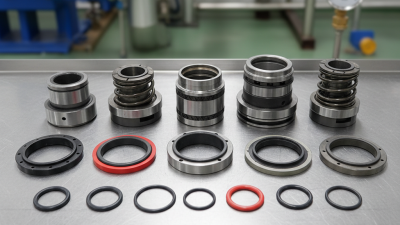
In 2026, global buyers need more than a low unit price when selecting Seal Components. They need dependable performance across different machines, climates, and supply chains. A small mismatch can cause leakage, downtime, product returns, or costly maintenance. Seal design should begin with real operating conditions, not a generic catalog image.
This guide explains how experienced purchasing teams evaluate material, profile, size, pressure, temperature, motion, and chemical exposure. It also considers installation space, service life, packaging, traceability, and supplier communication. A seal used in a hydraulic cylinder may require different properties from one installed in a food-processing pump. Exact drawings matter. So do samples, inspection reports, and documented test results. Qualified suppliers should explain their material grades and manufacturing controls clearly. Their claims should remain verifiable through technical data and consistent quality records.
No component is perfect. Supplier catalogs can omit critical limitations, and laboratory results may not reflect field conditions. That is why responsible buyers compare specifications with actual application evidence. They should confirm tolerances, request pre-production samples, and review performance after installation. Regional standards and customer requirements may also affect material selection and documentation. This article offers a practical framework for reducing uncertainty while building reliable international sourcing decisions. It does not replace engineering validation. Careful testing still matters.
Define the sealing application before comparing materials, profiles, or prices. Identify whether the seal handles static pressure, reciprocating motion, rotation, or frequent thermal cycling. Record the medium carefully, including oil, water, refrigerant, abrasive slurry, or process gas. A clean datasheet can still mislead.
Specify pressure peaks, continuous pressure, temperature range, shaft speed, stroke rate, and expected service life. Check chemical compatibility at the highest temperature, not only at room temperature.
The U.S. Department of Energy reports that compressed-air leaks can waste 20–30% of compressor output in poorly maintained systems. This makes leakage control an operating-cost issue, not merely a component choice.
For hydraulic equipment, pressure pulses and extrusion gaps often matter more than average pressure.
Measure the housing, groove, shaft, surface finish, and installation clearance. Confirm tolerance changes after heat exposure. In practical specification reviews, installation damage appears more often than buyers expect. That deserves attention.
Global buyers should also document cleaning agents, storage conditions, replacement intervals, and local maintenance skill.
ISO 3601 provides dimensional and tolerance guidance for O-rings, but it cannot replace application testing. A seal may pass a laboratory test and still fail after contamination, misalignment, or poor assembly. Pilot testing under real duty cycles remains the more reliable decision.
Selecting seal materials starts with the media, not the catalog price. Oils commonly suit NBR, while steam and hot water often require EPDM. FKM handles many fuels and elevated temperatures, but it may perform poorly with certain amines or hot steam. PTFE offers broad chemical resistance, yet its low elasticity can complicate low-pressure sealing.
Temperature ratings need careful interpretation. A compound listed for 200°C may not survive continuous exposure, pressure cycling, or rapid decompression.
Pressure also matters. High pressure can push a soft seal into the clearance gap, causing extrusion. Add a backup ring when the gap, pressure, or temperature exceeds the compound’s practical limit.
The 2024 Grand View Research industrial seals report projects market growth near 4.8% annually, reflecting broader demand for reliable sealing in energy, chemical, and process equipment. Growth does not remove engineering uncertainty.
Tips: Build a media-temperature-pressure matrix before selecting a material. Check concentration, pressure spikes, shaft speed, and installation damage. Use ASTM D2000 classifications and ISO 23936 guidance where relevant. NACE MR0175/ISO 15156 is important for sour-service applications. Laboratory testing with the actual fluid is safer than relying on a generic chart. Some choices still fail. I have seen temperature receive more attention than chemical concentration, which is often the hidden cause of swelling, hardening, or leakage.
2026 How to Choose Seal Components for Global Buyers?
Choose Seal Designs Based on Movement and Installation Needs
Seal selection should begin with movement, not price. Static seals suit flanges and covers. Rotary seals need controlled friction, shaft alignment, and wear resistance. Reciprocating seals face changing pressure and repeated sliding. These differences affect leakage, heat, and service life. The U.S. Department of Energy reports that poorly maintained compressed-air systems can lose 20–30% of their output through leaks. A small seal defect can become an expensive energy problem.
Installation conditions matter just as much. A cartridge design can reduce assembly errors in restricted spaces. A split seal may simplify maintenance around large shafts. Groove depth, surface roughness, temperature, pressure, and chemical exposure must match the application. ISO 3601 provides dimensional guidance for O-rings, but compliance alone does not guarantee performance. Field audits often reveal the same mistake: buyers select a material first, then discover the movement is wrong. That approach needs reconsideration.
Tips: Record speed, stroke length, pressure changes, temperature, and installation access. Ask for test data under similar conditions. Check shaft finish and alignment before ordering. Keep a replacement sample from the first approved batch. It saves time later.
For global buyers, seal selection begins with standards, not price. ISO Survey 2022 recorded more than 1.26 million ISO 9001 certificates worldwide. That figure shows quality systems are widespread, but certification does not prove sealing performance. Request current certificates, audit scope, manufacturing location, and material traceability.
Match the component to its working environment. ISO 3601 supports O-ring dimensions and tolerances, while ISO 23936 addresses non-metallic materials in petroleum applications. Food-contact assemblies may require FDA 21 CFR 177.2600 or EU Regulation 1935/2004 evidence. For pharmaceuticals, USP Class VI testing can support material suitability. Check temperature, pressure, fluid chemistry, extrusion gaps, and compression set. A certificate alone can mislead.
Grand View Research estimated the global industrial seals market at about USD 13.7 billion in 2023. Growth increases supplier choices, but compatibility data remains uneven. Ask for test conditions, not only pass-or-fail statements. Confirm whether results cover the actual compound, hardness, surface finish, and installation method. In practice, buyers often overlook storage aging and assembly damage. I would also challenge one assumption: a higher-grade material is not automatically safer. It may swell, harden, or fail under a different fluid. Small pilot tests and documented inspection criteria reduce that uncertainty.
Compare typical continuous service-temperature ranges before checking the applicable global standard, certification, fluid compatibility, pressure, and installation requirements. Values are indicative engineering ranges and vary by compound, design, and operating conditions.
Global buyer checklist: verify ISO 3601 for O-rings, ASTM D2000 for elastomer classification, EN 681-1 for certain water and drainage sealing applications, FDA 21 CFR 177.2600 for applicable rubber articles intended for repeated food contact, and EU Regulation (EC) No 1935/2004 where food-contact requirements apply. Certification suitability must be confirmed for the exact material compound and application.
Selecting seal components for global projects requires more than comparing unit prices. In supplier audits, I check material traceability, mold control, inspection records, and complaint handling. A capable supplier can show batch certificates and explain each test result clearly. Ask for samples from regular production, not specially prepared pieces. Measure hardness, dimensions, surface defects, and compression recovery. Small variations can become leaks after heat, pressure, or repeated movement. Request evidence from accredited laboratories when performance claims affect safety or reliability. Documents matter, but factory conditions matter too.
Cost needs a wider calculation. Include tooling, sampling, packaging, testing, customs preparation, and possible replacement losses. The cheapest quotation may hide unstable materials or weak process control. A spreadsheet helps, but it can still miss the cost of delayed production. Delivery risk deserves equal attention. Confirm raw material sources, production capacity, quality release timing, and backup plans. Ask how the supplier handles urgent changes or failed batches. Use agreed inspection points and realistic lead times. Do not accept promises without dated production schedules. I have seen buyers approve attractive prices before checking capacity during peak seasons. That choice often created pressure later. Leave room for uncertainty. Review supplier performance after every shipment, including defects, response time, and delivery accuracy. Keep the review factual, even when the relationship feels comfortable.
| Supplier Market / Supply Model | Typical Product Scope | Supplier Evaluation Score (100) |
Typical MOQ | Cost Index | Standard Lead Time | Expedited Lead Time | Main Quality-Control Evidence | Primary Delivery Risk | Recommended Buyer Action |
|---|---|---|---|---|---|---|---|---|---|
| East Asia High-volume export supplier |
O-rings, molded rubber parts, bonded seals, hydraulic and pneumatic sealing kits | 78–88 | 500–5,000 pcs | 70–90 | 4–8 weeks | 2–4 weeks | ISO 9001, material certificates, first-article inspection, AQL sampling, dimensional reports, batch traceability | Port congestion, production queue changes, and long ocean-transit exposure | Approve a production sample, define acceptance criteria, and hold safety stock for ocean shipments |
| South Asia Cost-focused manufacturer |
Standard elastomer seals, gaskets, washers, low-to-medium complexity molded components | 68–80 | 1,000–10,000 pcs | 65–85 | 6–10 weeks | 3–5 weeks | Incoming material inspection, production inspection, hardness testing, visual inspection, basic lot records | Variation in raw-material batches and limited capacity during peak periods | Require compound approval, test critical dimensions, and use dual sourcing for safety-critical parts |
| Europe Regulated or engineered supplier |
High-performance seals, engineered profiles, medical or food-contact components, low-volume precision parts | 86–95 | 100–1,000 pcs | 115–145 | 3–7 weeks | 1–3 weeks | ISO 9001, sector-specific quality systems, full material traceability, capability studies, validation reports, formal corrective action | Higher purchase price and possible capacity constraints for custom tooling | Use for regulated or failure-critical applications and compare total cost of ownership, not unit price alone |
| North America Short-lead-time regional source |
Replacement seals, custom molded parts, repair kits, prototypes, and urgent maintenance orders | 82–92 | 50–2,000 pcs | 105–135 | 2–6 weeks | 3–10 business days | Lot identification, dimensional inspection, certificate of conformity, documented nonconformance process | Higher labor cost and limited availability of specialized compounds or tooling | Select for urgent demand and service continuity; negotiate blanket orders to reduce unit cost |
| Nearshore Regional Source Shorter logistics route |
Standard and custom seals for automotive, machinery, fluid handling, and general industrial use | 75–87 | 250–3,000 pcs | 90–115 | 3–7 weeks | 1–3 weeks | Process inspection, material declarations, dimensional checks, sample retention, and shipment inspection | Cross-border customs delays and dependence on regional transport capacity | Confirm customs documentation, use agreed delivery terms, and maintain a backup route |
| Evaluation Dimension | Suggested Weight | What to Verify | Minimum Acceptance Guideline |
|---|---|---|---|
| Quality Management | 25% | Quality certification, inspection plans, nonconformance records, corrective-action response | Documented quality system and traceable batch records |
| Technical Capability | 20% | Material compatibility, tooling control, dimensional capability, testing equipment | Successful sample approval against drawing and application requirements |
| Total Cost of Ownership | 20% | Unit price, tooling, freight, duties, inspection, failure cost, inventory carrying cost | Lowest risk-adjusted cost, not simply the lowest quoted price |
| Delivery Performance | 15% | Capacity, production planning, historical on-time delivery, logistics options | Documented lead time and contingency plan for delays |
| Financial and Operational Stability | 10% | Capacity utilization, workforce stability, raw-material continuity, business continuity planning | Ability to support the contract throughout its expected life |
| Communication and Compliance | 10% | Response time, engineering support, export documentation, regulatory declarations | Clear technical communication and complete shipping documentation |